An Executive Guide to Medical Device Regulation (MDR), Industrial Automation Efficiency in China, Quality Auditing Standards, and Turnkey Production Ecosystems for Healthcare Enterprises.
Explore high-precision therapeutic device machinery, automated assembly systems, and Class I/IIa sterile packaging solutions built for global compliance.

In-depth analysis of regulatory shifts, risk classification under EU MDR 2017/745, and international quality management frameworks.
The global therapeutic equipment manufacturing sector is undergoing an unprecedented structural evolution driven by stringent international regulations, aging demographics, and escalating demand for non-invasive clinical interventions. Therapeutic devices—ranging from physical rehabilitation systems, hydro-pressure testing instruments, heat-coating medical tape machines, to automated fluid infusion production lines—serve as critical assets across hospitals, emergency care centers, and specialized therapy clinics. To achieve market access in the European Economic Area (EEA) and globally recognized jurisdictions, obtaining and maintaining CE Certification under the EU Medical Device Regulation (MDR 2017/745) has transitioned from a competitive advantage to an absolute prerequisite.
Under the EU MDR framework, the compliance burden for manufacturers and OEM/ODM sourcing partners has amplified significantly compared to the legacy Medical Device Directive (MDD). The regulation enforces rigorous post-market surveillance (PMS), unique device identification (UDI) traceability, and heightened clinical evaluation standards for active and non-active therapeutic equipment. Whether procuring Class I sterile wound dressing slitters or complex Class IIa/IIb automated assembly hardware, procurement directors must evaluate manufacturers based on their adherence to harmonized standards such as ISO 13485:2016 (Quality Management Systems for Medical Devices) and IEC 60601-1 (General Safety for Medical Electrical Equipment).
Key Strategic takeaway for Global Procurement Officers: CE Marking is not merely a stamp of compliance; it represents complete raw material traceability, verified bio-compatibility, validated cleanroom manufacturing protocols (ISO Class 7/8), and guaranteed electromagnetic compatibility (EMC) for all powered therapeutic devices.
Comprehensive quality management governing raw material sourcing, machining tolerances, contamination controls, and batch-level audit trails.
Exhaustive clinical evaluation reports, risk assessment dossiers under ISO 14971, and robust Post-Market Clinical Follow-up (PMCF) plans.
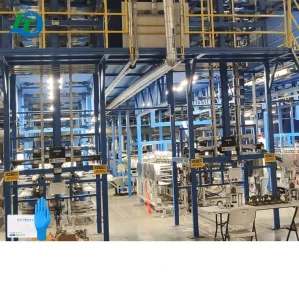
Automated assembly lines designed for zero-defect output, reducing contamination risks in sterile consumable production.
Why international healthcare brands and medical device buyers partner with specialized Chinese manufacturing hubs like Suzhou.
China has transformed from a low-cost contract manufacturing base into an advanced high-tech epicenter for medical device fabrication, automation, and pharmaceutical equipment engineering. The Yangtze River Delta region—anchored by industrial centers like Suzhou—houses a complete supply chain cluster spanning high-precision CNC machining, medical-grade polymer synthesis, sensor integration, and intelligent PLC control programming.
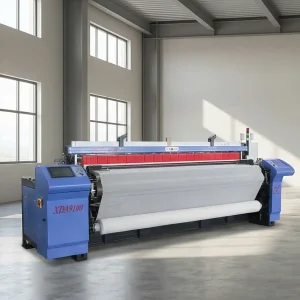
This geographic concentration creates unmatched supply chain velocity. When manufacturing therapeutic machinery such as IV catheter automated assembly lines, high-speed gauze jet looms, or vacuum sealing machines, Chinese manufacturers leverage local component availability to compress production lead times by 40% to 60% compared to Western counterparts. Furthermore, continuous capital investment in robotic assembly, automated optical inspection (AOI), and laser die-cutting ensures that unit-to-unit consistency meets micro-level tolerances.
From raw stainless steel grade 316L fabrication to multi-axis servo drive integration, the localized supply chain eliminates cross-border component bottlenecks, allowing custom OEM/ODM machinery to move from CAD design to factory acceptance testing (FAT) within record timelines.
By leveraging direct factory-gate procurement models, global distributors and healthcare institutions bypass multi-tiered intermediary markups. Capital expenditure is optimized, freeing up resources for localized marketing, clinical trials, and regulatory registration.
Your Trusted One-Stop Virtual Office and Strategic Sourcing Partner in China Since 2013.
Suzhou Hanora Medical Supplies Co., Ltd. was founded in 2013. We are a premier sourcing company focusing on high-grade medical devices, therapeutic machinery, and laboratory equipment. We are deeply committed to providing our global clients with seamless, one-stop sourcing services—effectively acting as their dedicated virtual office in China.
Our comprehensive operational scope encompasses end-to-end management: product sourcing, authentic price negotiation, rigorous supplier verification, thorough factory auditing, continuous production monitoring, standardized laboratory testing, strict order follow-up, multi-stage quality control, pre-shipment inspections (PSI), and reliable logistics support.
Having successfully exported high-performance equipment to more than 30 countries, our team brings vast international trade expertise. For our global client partners, we guarantee: the prices we offer are 100% authentic factory-gate prices, and clients are always empowered to pay directly to the manufacturing facilities.
Corporate Social Responsibility: Beyond commercial excellence, we care deeply about societal welfare. We proudly pledge 5% of our net profit to charitable initiatives to help impoverished communities and build a better world.
For new clients, we provide free product sourcing evaluations for up to 3 distinct product lines, delivering complete quotation proposals within 1-2 business days.
Eliminate intermediary financial friction. We facilitate flexible, secure payment gateways allowing buyers to transfer funds direct to audited factories.
All-rounded auditing: verifying corporate credentials, checking customs export records, conducting on-site operational visits, and executing strict pre-shipment checks.
Deploying experienced representatives directly to factories to negotiate long-term contract agreements, framework terms, and special technical specifications.
Leveraging our extensive supplier matrix to manage customized OEM/ODM projects, prototyping, mixed-model container shipping, and specialized machine adjustments.
Partnered with leading international freight forwarding networks, providing seamless sea, air, and multimodal transport quotes alongside custom clearance assistance.
How CE certified therapeutic production lines cater to diverse clinical, institutional, and commercial environments.
High-volume production lines for sterile IV catheters, surgical sponges, and wound dressings support critical care units where zero defect tolerance is mandatory.
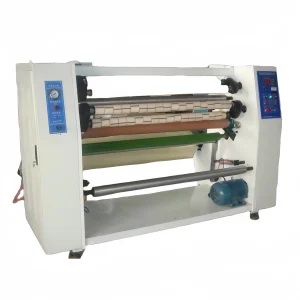
Precision thermal coating machinery crafts therapeutic adhesive tapes and kinesiology dressings designed for post-surgical recovery and muscle alignment.
Automated nursing pad packaging systems and glove manufacturing lines provide essential protective barriers for eldercare facilities and home healthcare programs.
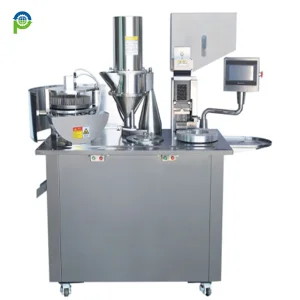
Advanced pharmaceutical blister packaging, hydrostatic pressure testing instruments, continuous slitting systems, and syringe molding setups.




Navigating the convergence of artificial intelligence, green biocompatible materials, and smart factory connectivity.
Integration of computer vision and machine learning models directly into flow packers and slitting lines to detect sub-millimeter defects in real-time.
Adapting plastic injection moulding and coating hardware to handle biodegradable PLA and eco-friendly non-wovens while maintaining CE safety compliance.
Smart therapeutic machinery equipped with OPC-UA protocols for real-time operational efficiency monitoring, predictive maintenance, and remote auditing.
Expert answers regarding CE certification, factory audits, direct payments, and technical equipment testing.
 Hanora Medical